Project Background & African Market Insights
Kenya stands as one of the largest and most progressive dairy markets in Sub-Saharan Africa. However, the country's unique geographical climate and underdeveloped cold-chain logistics present significant challenges for fresh milk distribution. To overcome these logistical barriers and supply safe, long-shelf-life dairy products to both urban and remote regions, a prominent Kenyan dairy enterprise decided to invest in a state-of-the-art, fully automated Ultra-High Temperature (UHT) aseptic milk factory.
The client selected Weishu Intelligent Machinery as their trusted EPC partner to solve several localized operational challenges:
-
Extended Shelf Life Without Refrigeration: The production line had to guarantee commercial sterility, allowing milk to be stored safely at ambient temperatures for up to 6 months.
-
Fluctuating Local Power Grids: The equipment needed high operational stability and smart power-backup capabilities to withstand local voltage fluctuations.
-
Water and Energy Scarcity: Given the resource constraints in East Africa, minimizing water and electricity consumption during processing and cleaning was a top priority.
Project Scale at a Glance:
-
Raw Material: Liquid cow's milk processing of 100,000 Liters per Day (L/D).
-
Final Product: Aseptic UHT milk in brick cartons and pouch packaging.
-
Delivery Scope: Turnkey EPC solution by Weishu Intelligent Machinery (Engineering design, factory layout, core equipment fabrication, African logistics, on-site installation, and raw milk process debugging).
Advanced Technical Solutions & Core Equipment
To ensure commercial sterility while preserving the natural taste and texture of Kenyan milk, Weishu’s engineering team deployed an eco-friendly, highly automated processing system:
Weishu Tubular UHT Sterilizer (The Heart of the Line)
To eliminate all spoilage microorganisms and spores, we integrated the signature Weishu Tubular UHT Sterilizer.
-
Precise Thermal Processing: The system heats the milk to 137°C–142°C and holds it for exactly 4 seconds, followed by flash cooling. This rapid "ultra-high temperature" processing destroys harmful bacteria while protecting the milk's essential proteins, vitamins, and natural flavor from heat degradation.
-
High-Level Heat Recovery: The sterilizer features a multi-section heat regeneration design, recovering up to 90% of the thermal energy to preheat incoming raw milk, drastically lowering boiler fuel consumption.
Weishu Aseptic Surge Tank & Filling Integration
Between sterilization and packaging, the milk is held in a Weishu Aseptic Surge Tank.
-
The tank maintains a constant positive pressure using sterile air, completely preventing any ambient air re-contamination.
-
It interfaces seamlessly with advanced multi-layer aseptic carton filling machines, ensuring zero-human intervention from the sterile piping to the sealed carton.
Smart Automated CIP (Clean-in-Place) System
To maintain the highest hygienic standards without wasting local resources, Weishu designed a localized intelligent CIP system.
-
The system utilizes a split-tank design that recycles final rinse water for the initial flush of the next cycle, reducing fresh water consumption by 35%.
-
Automated acid/alkali dosing guarantees a consistent chemical concentration, eliminating human error and ensuring 100% reliable sanitation.
African Field Execution & Cross-Border Delivery
Shipping heavy industrial machinery to East Africa and ensuring a smooth startup requires profound international expertise. Weishu’s global execution team managed the entire lifecycle seamlessly:
-
Robust Engineering for Local Conditions: All electrical cabinets fabricated by Weishu were equipped with heavy-duty voltage stabilizers and surge protectors tailored to the local Kenyan grid characteristics.
-
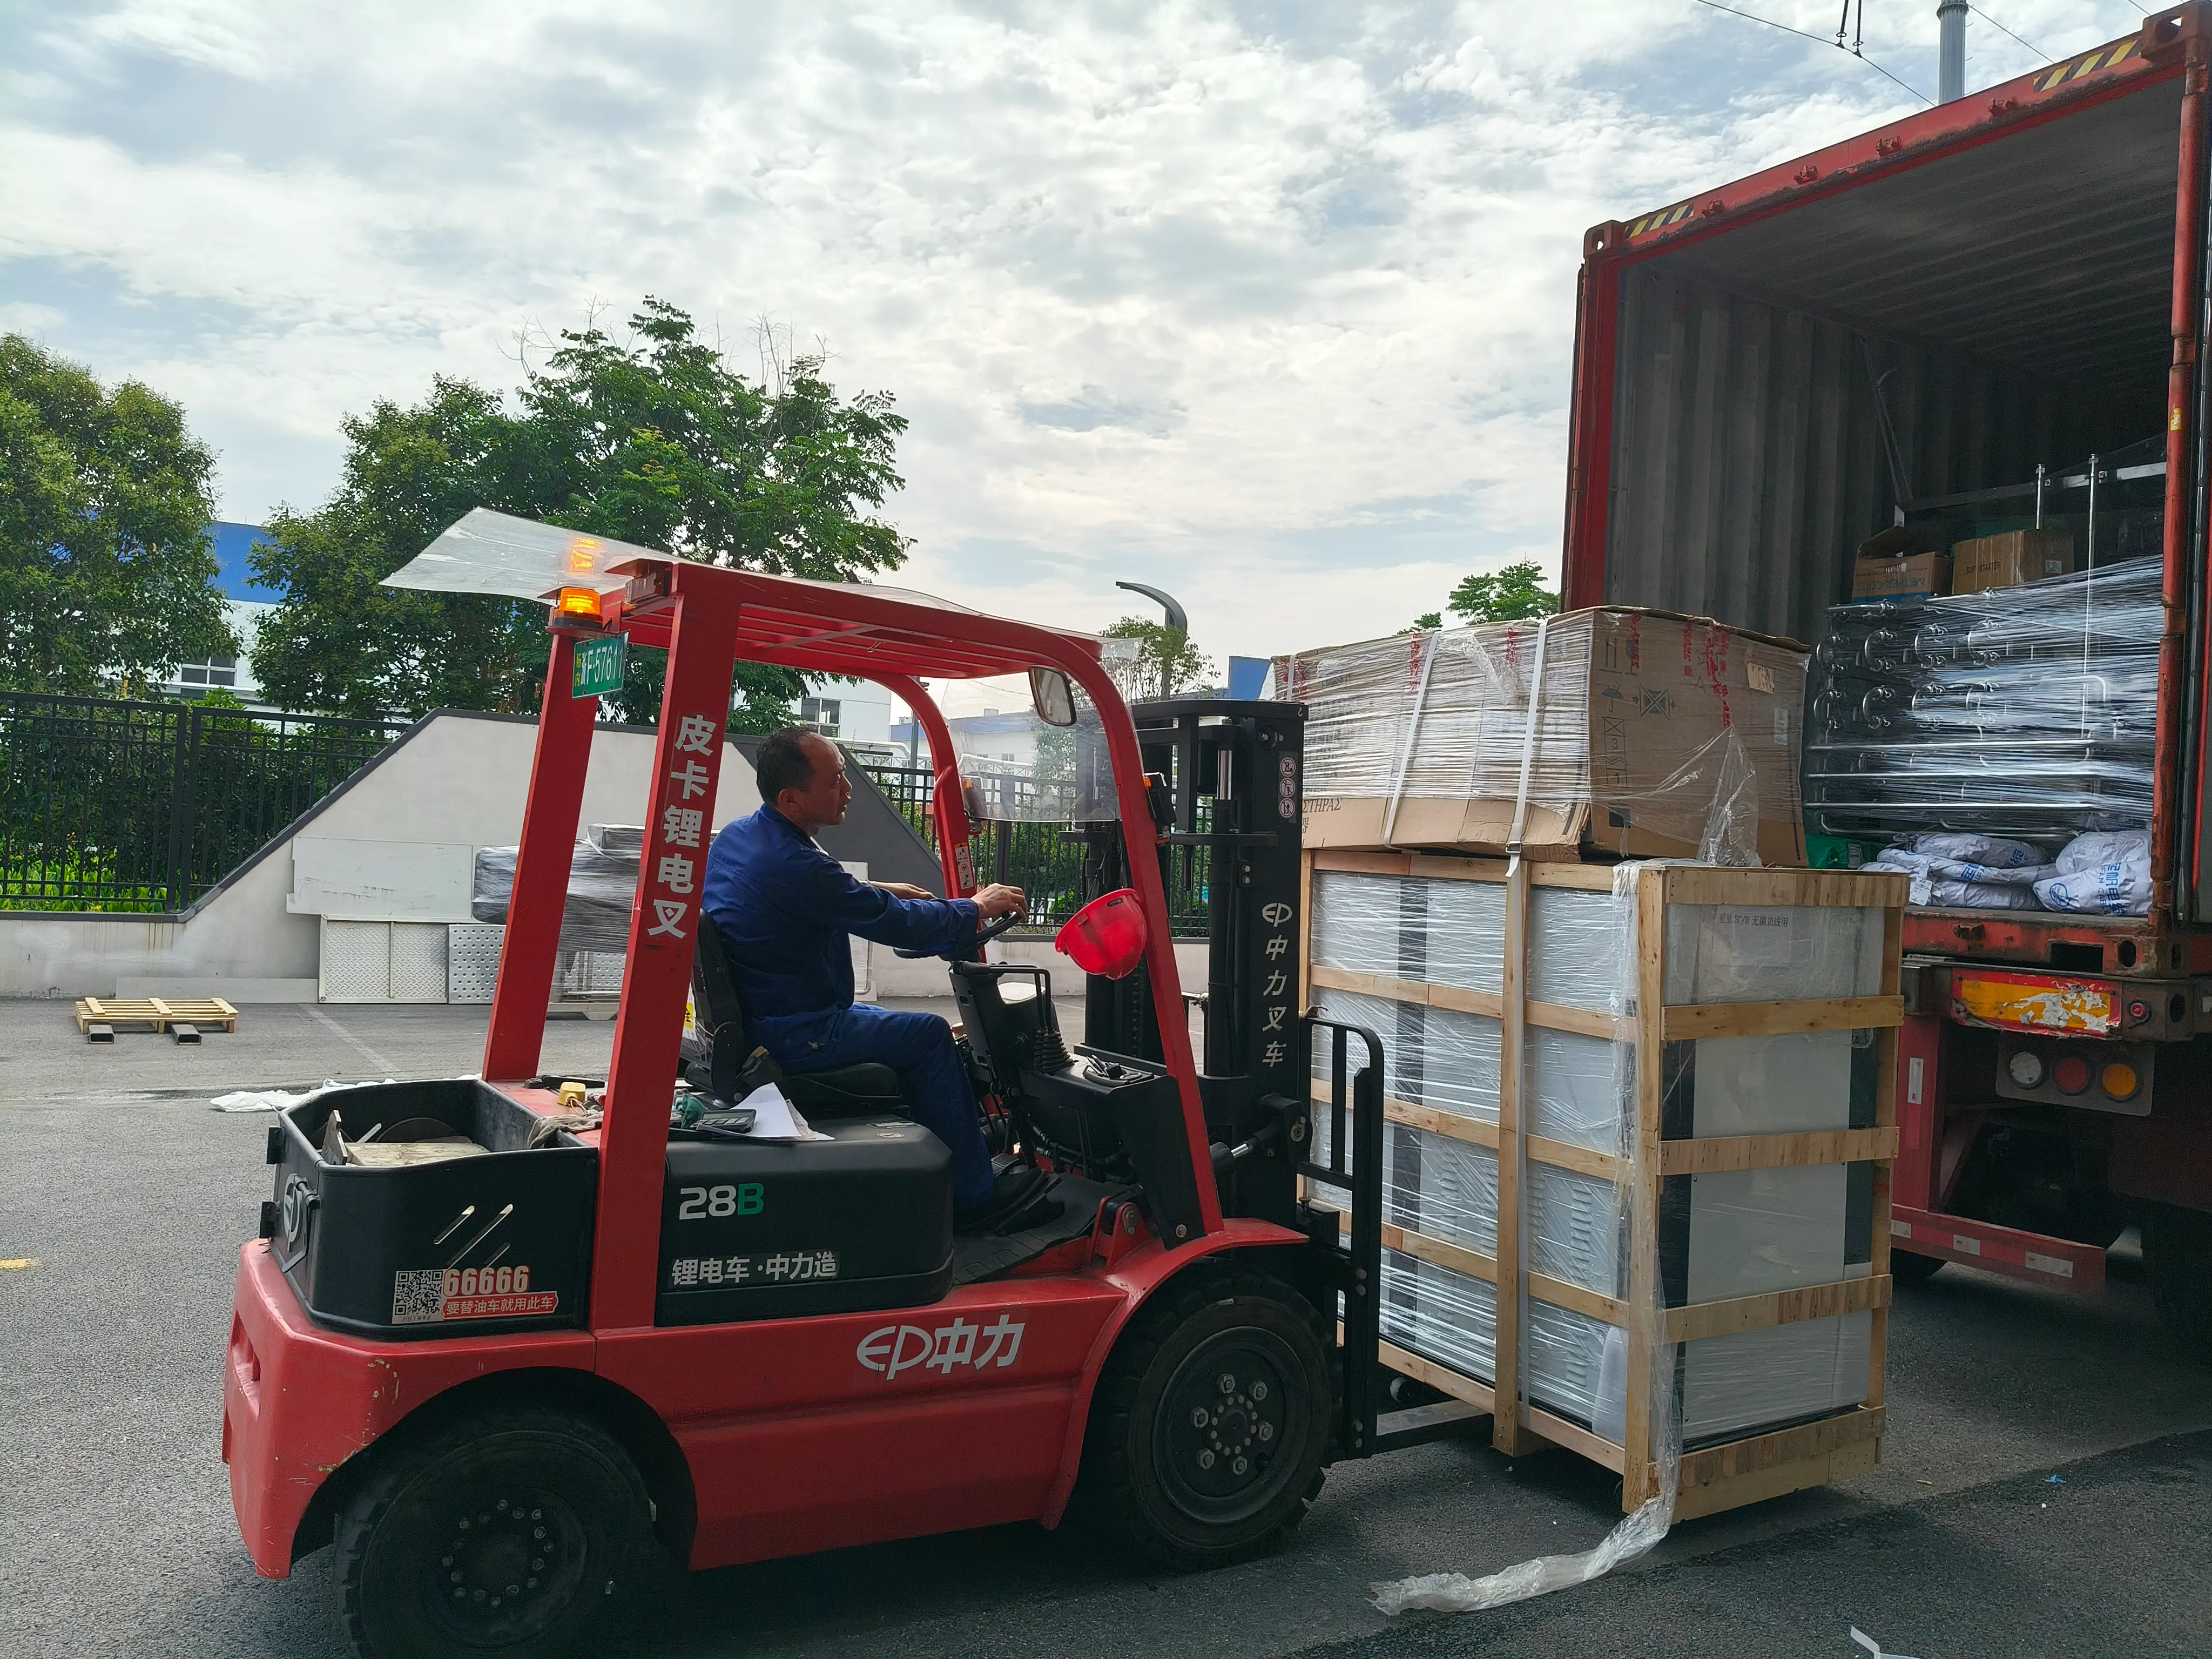
Door-to-Port Logistics Management: Weishu coordinated the complex sea freight to the Port of Mombasa and managed the inland transit to the inland factory site, ensuring all delicate automation sensors arrived completely intact.
-
Experienced Commissioning Engineers on Site: A dedicated team of Weishu field engineers spent weeks on-site in Kenya. They successfully managed the mechanical positioning, sanitary pipe orbital welding, and PLC software integration.
-
Empowering the Local Workforce: We provided intensive, hands-on technical training to local Kenyan operators. The training focused on aseptic operations monitoring, critical control point (HACCP) management, and routine maintenance, establishing a self-sufficient local team.
Quantifiable Business Outcomes
The successful launch of the 100,000 L/D aseptic milk line has completely transformed our client’s business model and market reach:
-
0% Contamination Rate: The factory achieved perfect commercial sterility, with 100% of finished batches passing rigorous aseptic incubation tests.
-
30% Reduction in Utility Costs: Thanks to Weishu’s thermal recycling design and water-saving CIP system, the plant’s overall utility expenditures dropped by 30% compared to standard regional setups.
-
Nationwide Distribution Network: With a reliable 6-month ambient shelf life achieved, the client expanded their distribution from localized regions to supermarket chains across Kenya, Uganda, and Tanzania.
-
Enhanced Brand Equity: The premium, consistent quality of the UHT milk positioned our client as a leading trusted dairy brand in East Africa.
Conclusion
The successful handover of this UHT dairy plant in Kenya highlights Weishu Intelligent Machinery’s capability to deliver world-class, resource-efficient engineering solutions in developing and challenging environments. We don't just export machinery—we build the infrastructural foundation that enables global food brands to overcome logistical boundaries and thrive.



 EN